 简体中文版

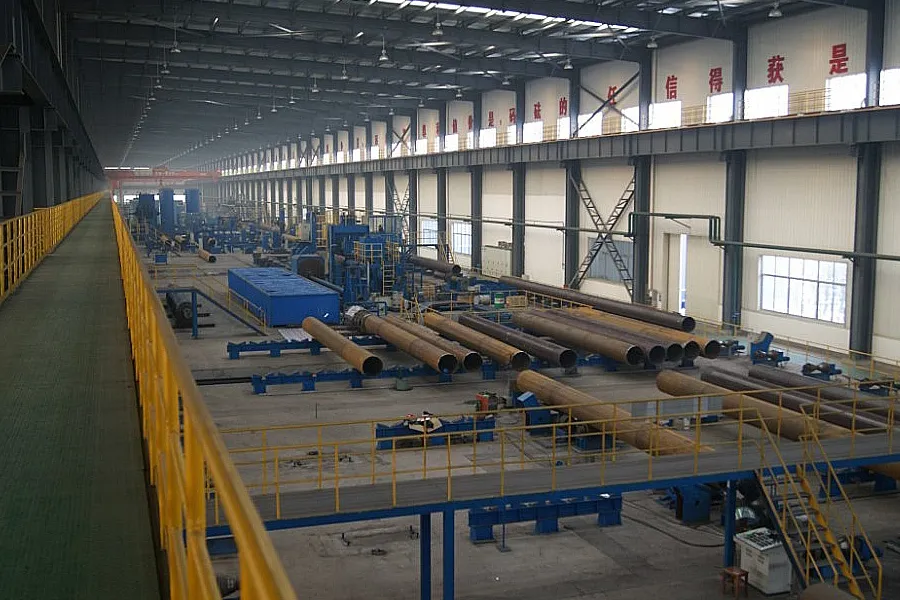
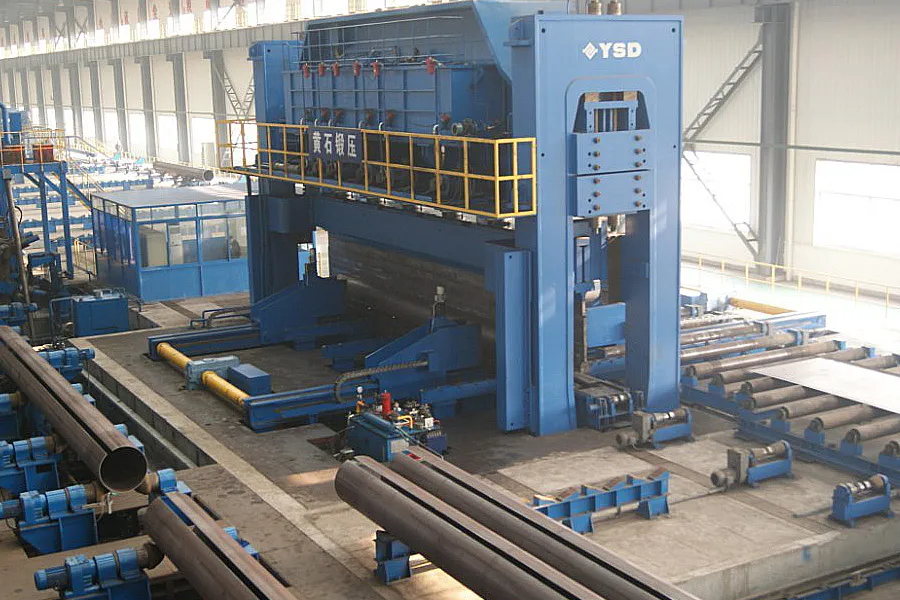
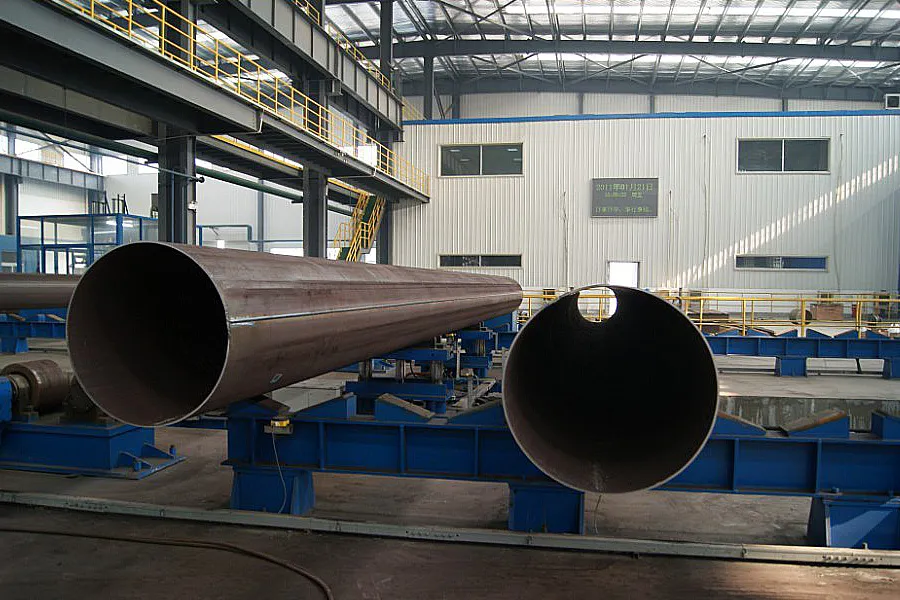
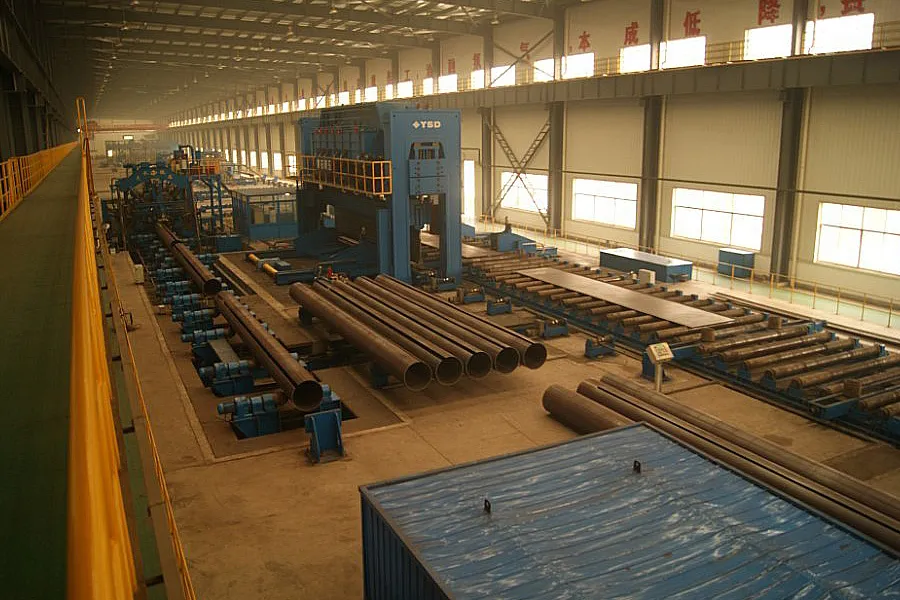
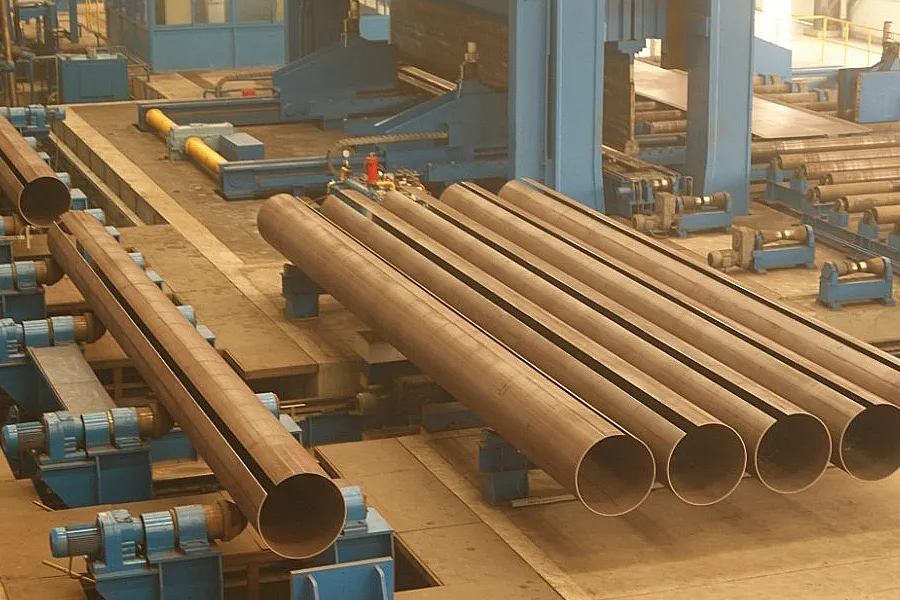
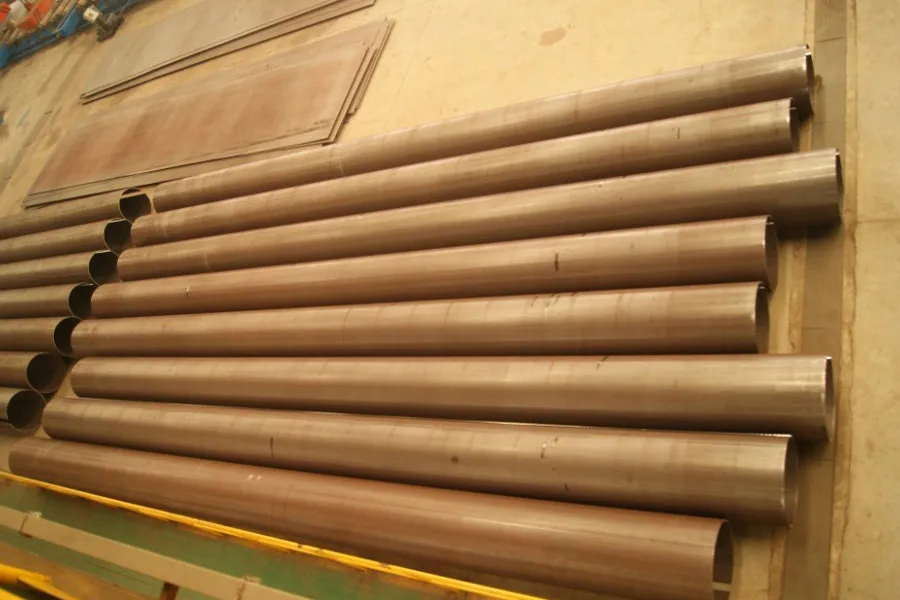
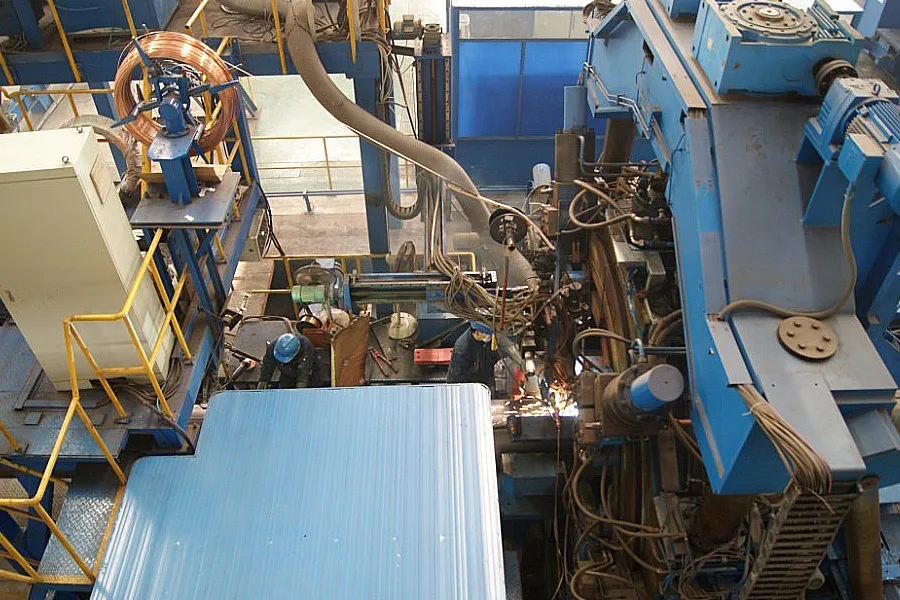
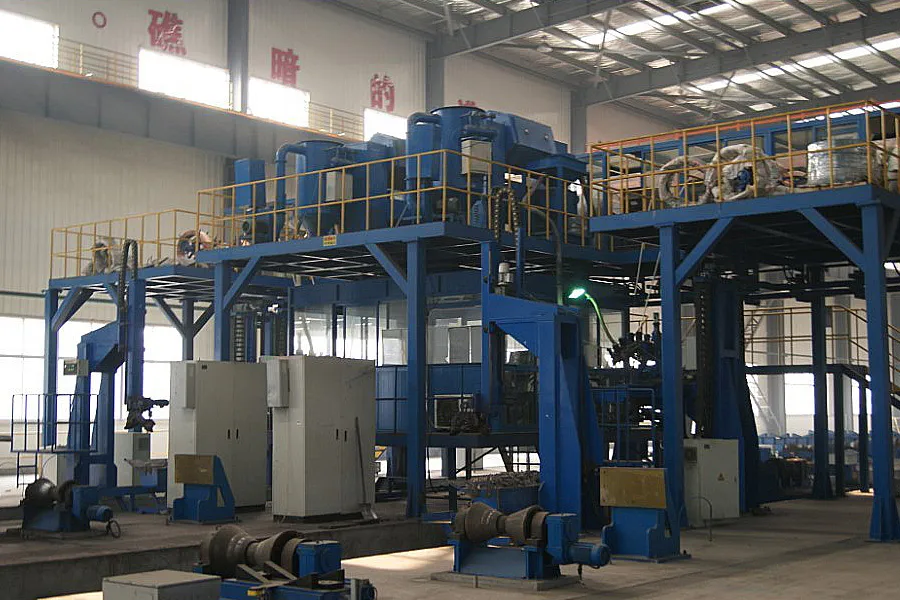
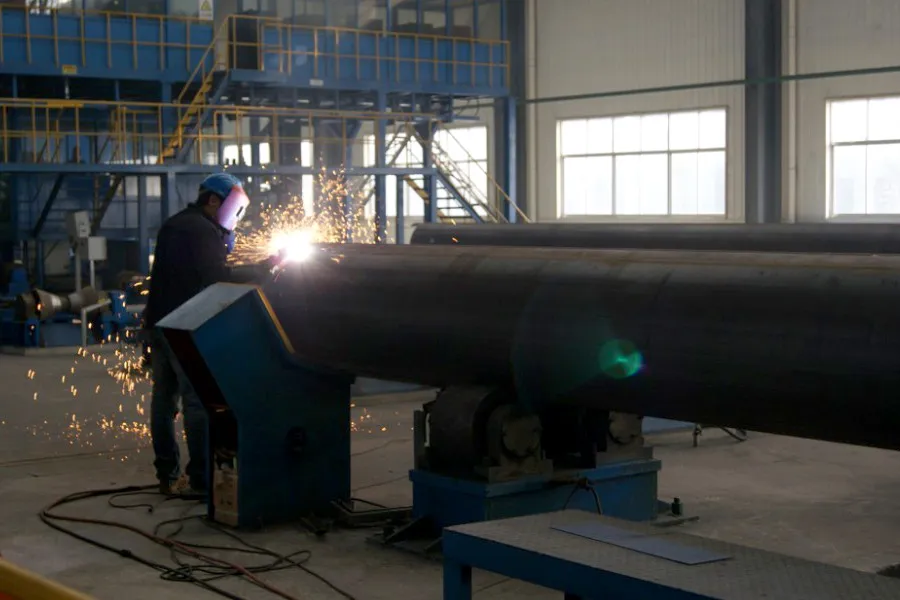
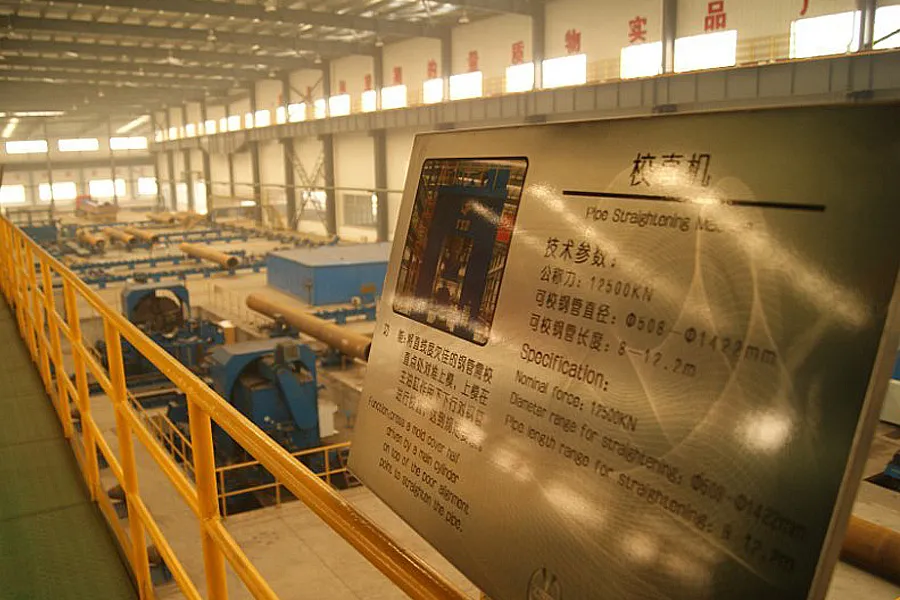
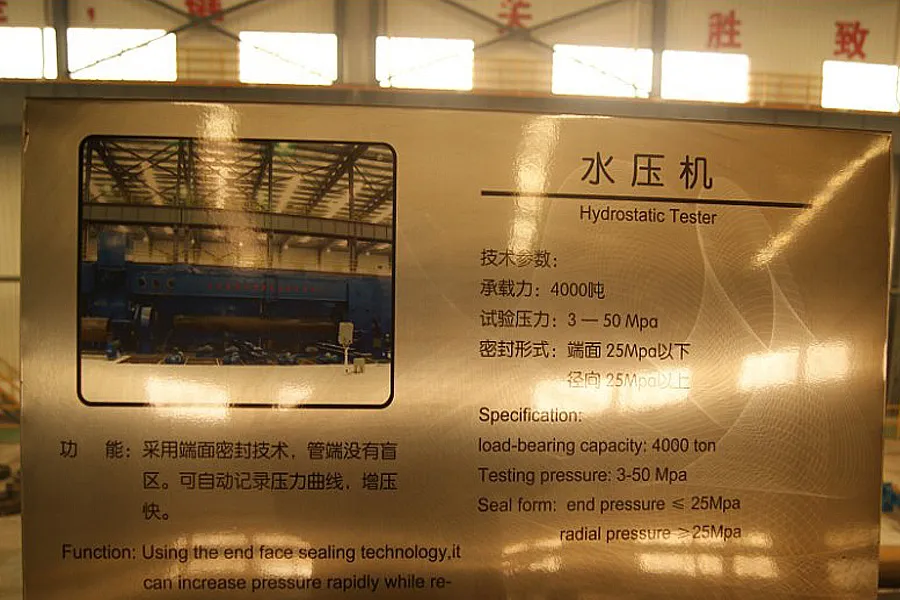
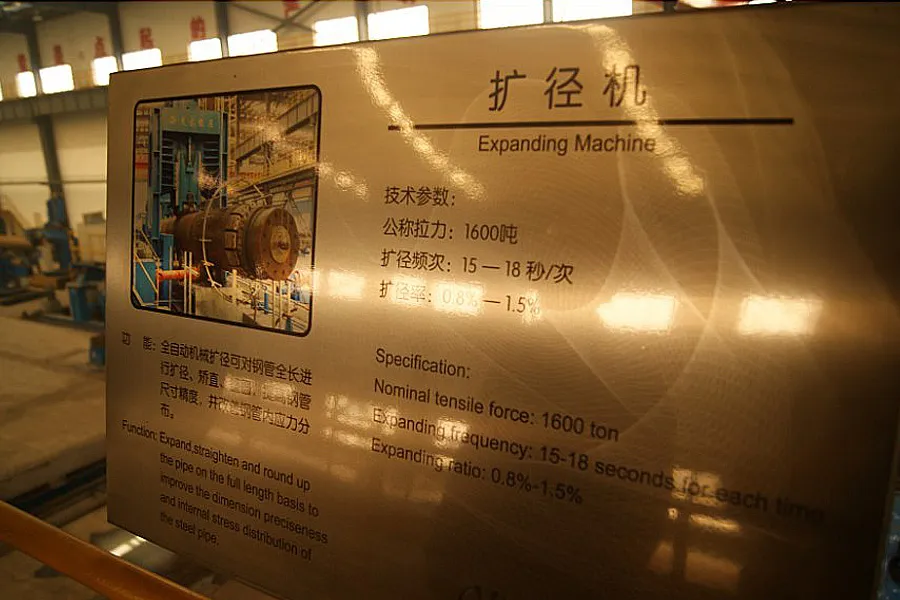
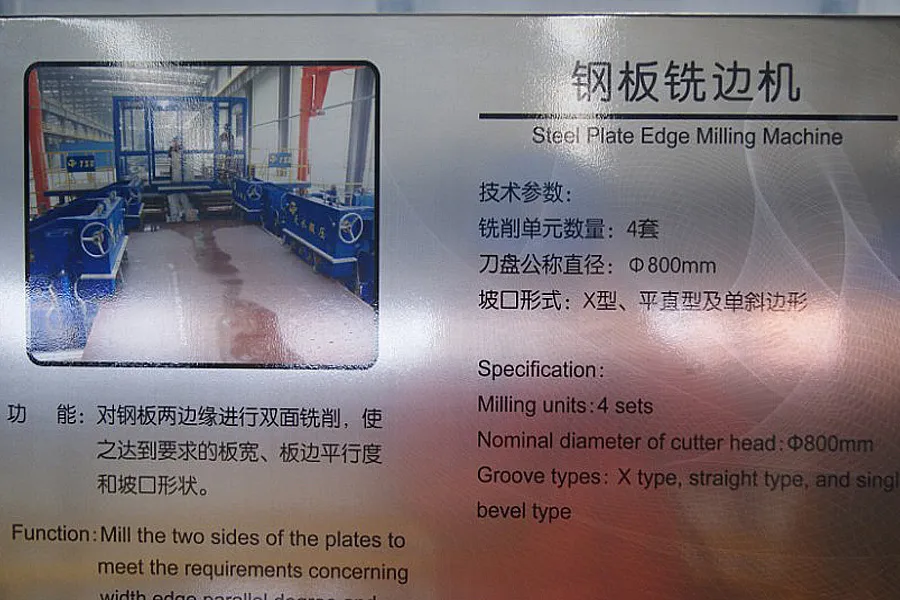
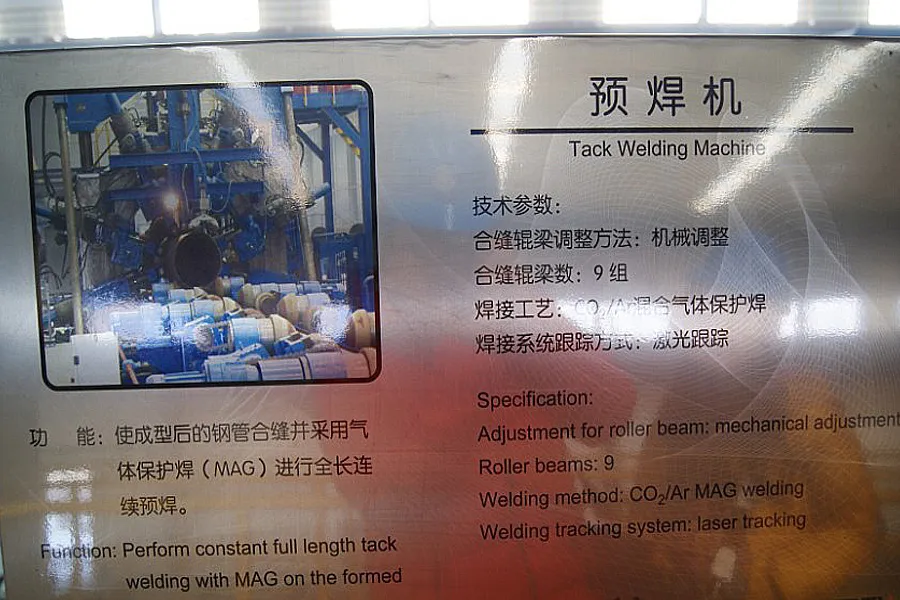
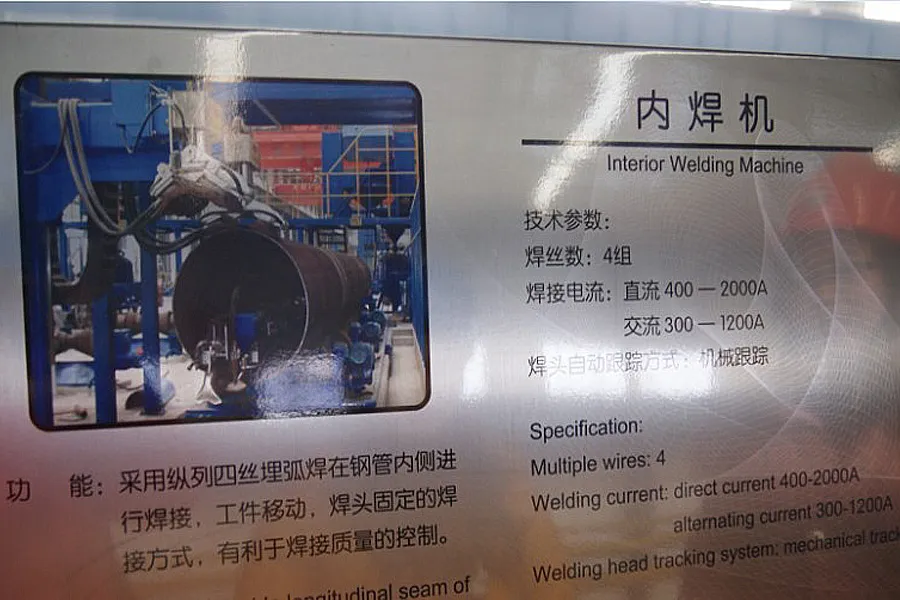
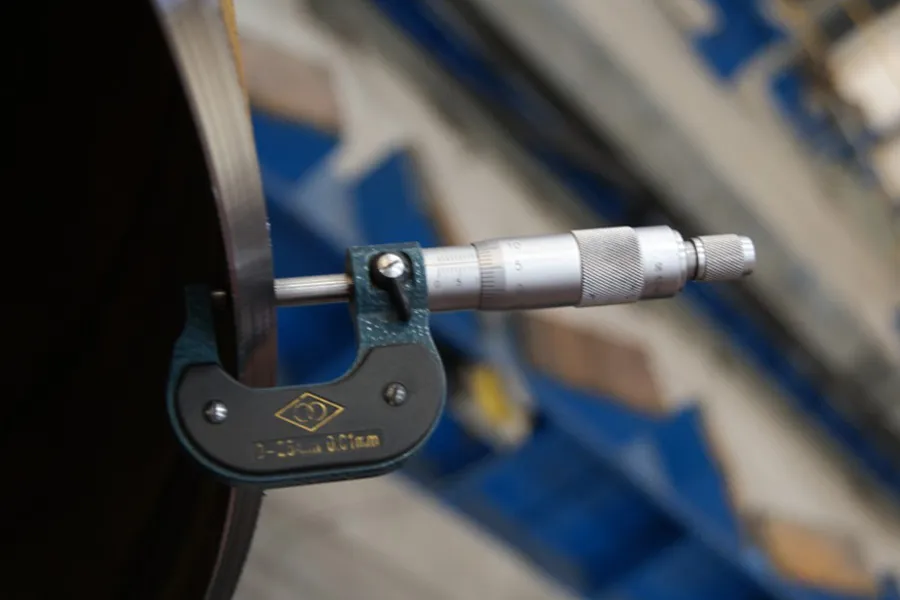
Huaxi's LSAW steel pipe production line manufactures steel pipes by forming steel plate into a cylindrical shape and joining the longitudinal seam through submerged arc welding. This process is widely used for large-diameter pipes and applications requiring substantial wall thicknesses, including oil and gas transmission, water infrastructure, and foundation piling.
1) Dimensional Range
| Item | Specification |
|---|---|
| Outside Diameter | 406.4–1422 mm (16–56 in) |
| Wall Thickness | 8–50 mm |
| Pipe Length | 6–12.5 m; other lengths subject to confirmation |
2) Applicable Standards: API 5L, ASTM A252, EN 10219, ASTM A53, GB/T 9711, subject to product type and order requirements.
3) Available Steel Grades: API 5L Grade B, X42, X52, X60, X65, X70, X80; ASTM A252 Grades 2 and 3; S235JRH, S275J0H, S355J2H, and S460, subject to the applicable standard and product specification.
4) Primary Applications
Huaxi's LSAW pipes are used in oil and gas transmission, water infrastructure, offshore and marine engineering, and structural foundation projects, including port construction and bridge piling.
The main manufacturing stages of LSAW steel pipes are outlined below.
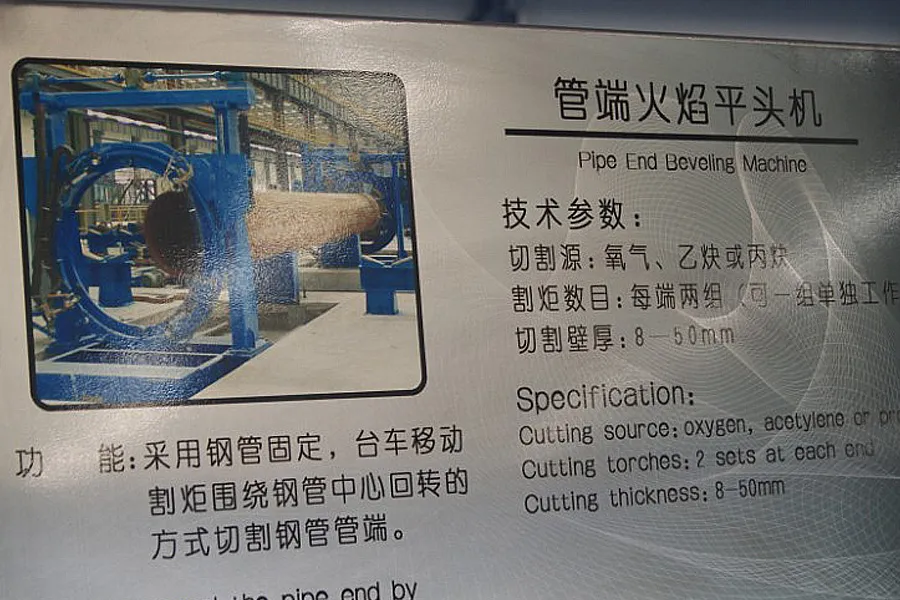
Steel plate preparation includes surface cleaning, edge milling, and beveling to prepare the plate for forming and longitudinal welding.
The edges of the steel plate are pre-bent to match the required pipe diameter before the plate enters the forming stage.
The plate is formed by the JCO process — progressive press bending in J-C-O steps — then closed into an O-shape with an open seam, followed by inside and outside submerged arc welding and mechanical expansion (JCOE).
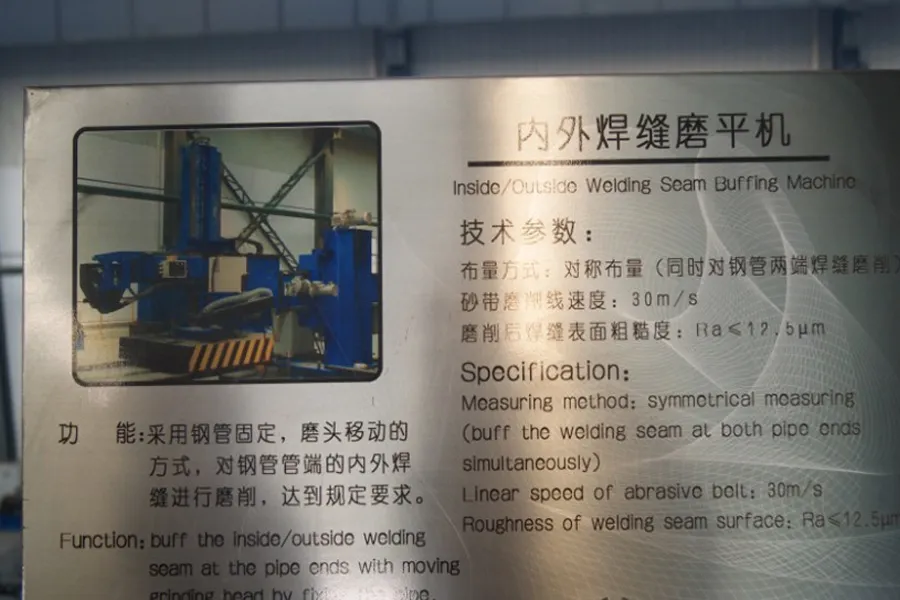
The longitudinal seam is welded by submerged arc welding, with welding passes applied to the inside and outside of the pipe.
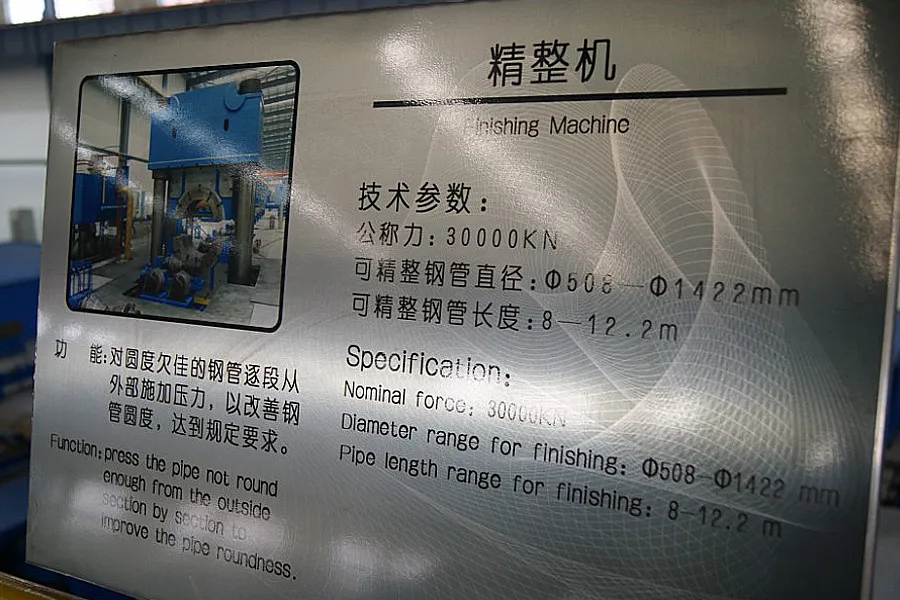
The welded pipe undergoes mechanical expansion to achieve the specified diameter and roundness.
Dimensional inspection, weld NDT (UT / X-ray), and hydrostatic testing from 3 to 50 MPa per API 5L, ASTM A252 or EN 10219, as specified in the order.
Huaxi's LSAW pipe production focuses on dimensional accuracy, welding parameter control, and production planning.
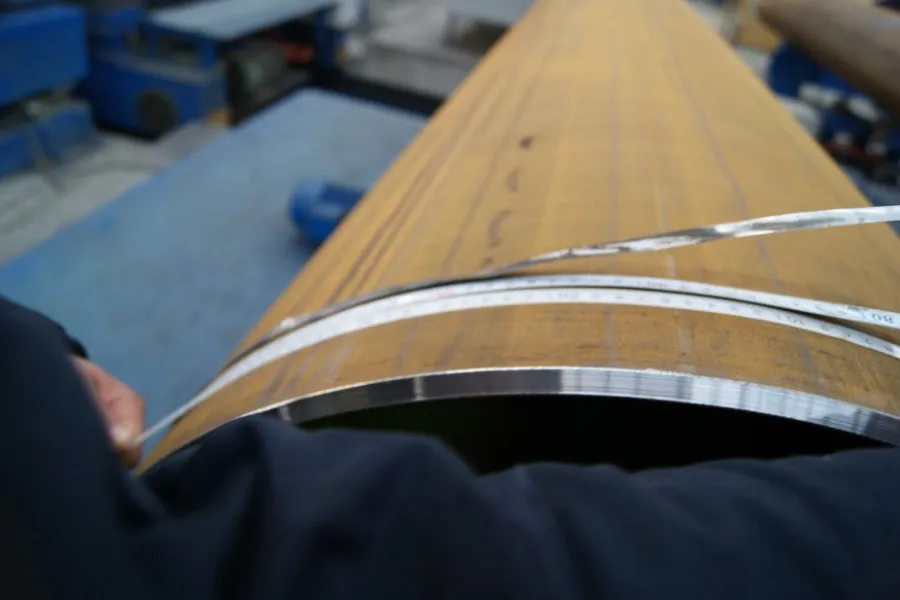
Dimensional Control: Pipe diameter, wall thickness, roundness, and straightness are controlled during forming and sizing to meet specified dimensions and tolerances.
Welding Control: Welding parameters are managed according to the applicable welding procedure and product specification.
Production Planning: Pipe dimensions, steel grades, and order quantities are coordinated with production requirements and delivery schedules.
LSAW pipe inspection covers material verification, weld testing, final product checks, and inspection documentation according to the applicable standards and order requirements.
Material Verification: Material certificates are checked against the specified steel grade and order requirements.
Weld Inspection and Testing: Welds are examined using the non-destructive testing methods required by the applicable specification. Hydrostatic and mechanical tests are conducted where specified.
Final Inspection: Finished pipes are checked for compliance with the specified product requirements before dispatch.
Inspection Documentation: Inspection results and material records are compiled according to the order requirements.
LSAW pipe orders can involve different dimensions, steel grades, inspection requirements, and delivery specifications. Huaxi coordinates these requirements for each order, from production planning to final marking and packaging.
The LSAW line has supported overseas projects where large-diameter welded pipe is the load-bearing, pressure-bearing element.
Deep Sea Gas Field Project — Nigeria
Scope: deep sea oil & gas development, deep-seam submerged-arc welded pipe rated for deep-water service (approximately 350× atmospheric pressure).
- Application: offshore gas field development under deep-water conditions
- Supply: submerged-arc welded pipe for the deep-water environment
- Technical requirements: pressure resistance suited to deep-sea service
- Delivery: project-specified welded pipe, documentation and shipping coordination
Address:1177 Huanhu Road, Yuelu District, Changsha, Hunan, China
 WhatsApp
 WeChat